Analyzing the strategic demand for resilient, energy-efficient high-bay illumination in Serbia's capital and surrounding industrial zones.
The Belgrade Industrial Landscape
Belgrade, as the financial and logistical epicenter of the Western Balkans, is currently undergoing an unprecedented modernization process. Driven by major infrastructure expansions around the Danube and Sava river basins, expanded intermodal freight terminals, and the rapid expansion of industrial parks in Šimanovci, Dobanovci, and Batajnica, the region demands high-performance lighting infrastructure.
Industrial facilities in Belgrade face severe microclimatic challenges. High humidity from surrounding waterways, significant seasonal ambient temperature fluctuations (-15°C in winter to +40°C in summer), and heavy airborne dust load in manufacturing plants demand lighting systems with exceptional thermal management and dynamic sealing technology. Standard indoor fixtures frequently fail under these aggressive ambient stress conditions.
Procurement Shift Toward Eco-Design & Resilience
With Serbia aligning its energy framework with EU green energy mandates and decarbonization goals, municipal and private enterprise procurement strategies in Belgrade have shifted dramatically. Facility managers no longer evaluate fixtures on initial capital expenditures (CAPEX) alone; the operational expenditures (OPEX), Total Cost of Ownership (TCO), and system reliability take top priority.
Key Procurement Metrics in Belgrade: High luminous efficacy (>180 lm/W), IP66/IP65 water and particulate resistance, robust transient surge protection (10kV/12kV), and full compliance with European CE, RoHS, and LVD directives.
Deep-dive into structural casting, thermodynamic management, and optic technology engineered for high-bay lighting applications.
ADC12 Die-Cast Aluminum Matrix
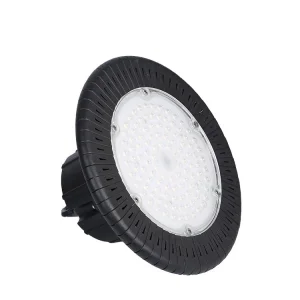
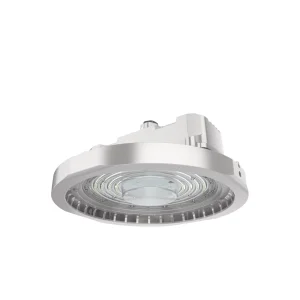
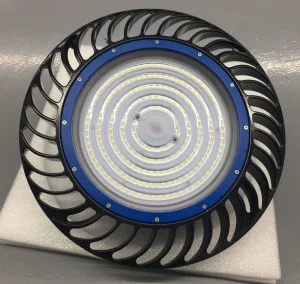
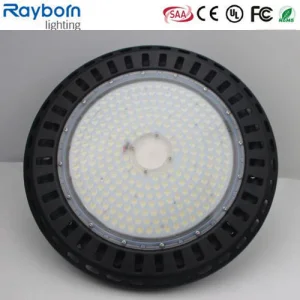
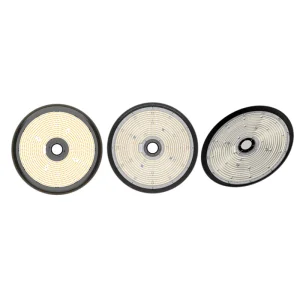
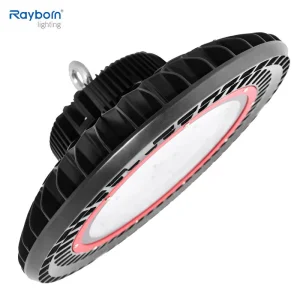
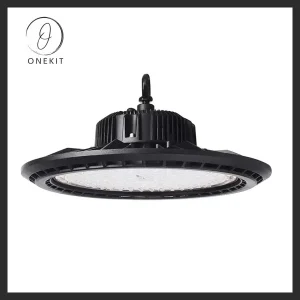
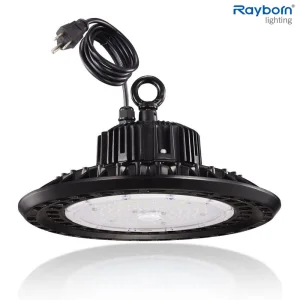
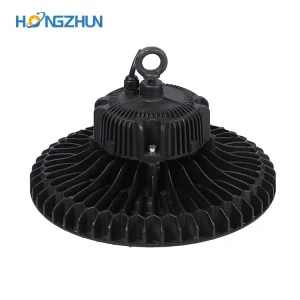
Our industrial UFO high bay lamps utilize premium ADC12 grade aluminum alloys processed through high-pressure precision casting. This produces a structural frame with exceptional mechanical strength and a thermal conductivity rating exceeding 96 W/m·K. The housing functions as an integrated high-surface-area heat sink, dissipating heat away from the LED engine rapidly to prevent junction temperature degradation.
Polymer Gasket Sealing & IP Rating
True waterproofing requires meticulous gasket design. Utilizing automated robotic dispensing, high-tier continuous silicone polymer rings seal the housing, lens matrix, and driver cavity. This guarantees an IP65 to IP66 ingress protection standard, completely blocking pressurized water jets, oil mist, airborne particulates, and high humidity condensation encountered in food manufacturing and chemical handling facilities.
Optic Precision & Glare Control
Equipped with optical-grade PC (Polycarbonate) lenses or tempered anti-glare micro-prismatic glass covers, our high bay lights offer multi-angle light distribution options (60°, 90°, 120°). This optical customization ensures uniform visual illumination across elevated multi-tier pallet racking systems in Belgrade logistics complexes, reducing visual fatigue for warehouse machinery operators.
Direct manufacturer insights: State-of-the-art production, automated optical testing, and end-to-end quality control.
Our company is a lighting enterprise specializing in the development, production and sales of IP66, IP65 Tri-proof light and indoor and outdoor ceiling lamps. We always adhere to the scientific management concept of "Credit from Sincerity, Business from Quality, People First" and constantly inject new vitality into the enterprise based on scientific and technological reform. We have a passionate and dynamic team; advanced research and development, automated production and testing equipment and mature production technology at home and abroad.
Our company has an independent mold research and development center and photoelectric testing equipment. In addition, we have our own darkroom, and advanced measuring instruments such as integrating sphere spectrometer, IP waterproof level tester, etc. We have introduced a large number of advanced instruments and equipment every year as a high-tech enterprise specializing in LED lighting application integrating product development, production, and sales. At present, our company has passed BSCI certification and ISO9001: 2000 quality system certification and our lighting products have passed the certification of TUV GS, CE, ROHS, LVD, EMC which will increase every year to make our certification system more complete.
Our company has continuously introduced LED lighting products with novel style, energy saving, environmental protection and practicality. Our products are exported to Europe, America, Southeast Asia, Australia, the Middle East, Africa, etc. Our annual production capacity can reach 3 million sets, with annual sales of 100 million, which is increasing at a steady pace every year.
Our IP66, IP65 Tri-proof light can be used in bathrooms, saunas, kitchens, hospitals, canteens, military barracks, bakeries, various material warehouses and production workshops, assembly workshops and other indoor places and some outdoor areas which require Moisture proof, waterproof and dustproof including swimming pools, squares, parks, camping, coal mines, aisles, tunnels, subways, underground parking lots, bridges, river banks docks, etc. According to the requirements of customers, our company will provide products with beautiful design, scientific and high quality. In the future, Ledlot Lighting will continue to improve and innovate, and strive to develop and create the unique core competitiveness of Ledlot!
Customization Engineering
We have our own specialized R&D team, and we can seamlessly develop and produce bespoke LED high bay products according to the complex engineering drawings or physical samples offered by our clients.
Cost Control & Optimization
We operate our own automated injection molding workshop and complete luminaire assembly workshop. Supply chain integration allows rigorous cost control with superior finished quality and highly competitive factory-direct pricing.
Strict Quality Verification
We feature advanced and complete internal inspection equipment, including integrating spheres, IPX6 water immersion chambers, and high-voltage surge testers to ensure pristine quality on every batch shipment.
Manufacturing Multiformity
We master injection molding, blister molding, and compression molding processes for lamp housings, accommodating diverse physical geometries, lengths, optics, and custom client branding requirements.
High Volume Capacity
With annual production sales reaching 100 million RMB and 3 million completed units, our massive throughput capacity effortlessly fulfills large-scale public infrastructure and global enterprise order demands.
Global Logistics Advantage
Our strategically situated production complex is located only 38 kilometers away from the Ningbo Port, allowing highly efficient, low-cost sea freight logistics and fast turnarounds for shipments bound for European ports.
Industrial Deployment Scenarios in Greater Belgrade
Tailored engineering configurations designed to solve specific operational challenges across key local sectors.
1. Cold Storage & High-Humidity Logistics
Located near the Danube freight routes, refrigerated logistics hubs face heavy condensation during daily door-cycling. Our IP66 UFO High Bay lamps use hydrophobic optical coatings and dual-chamber pressure equalizing breather valves that prevent moisture ingress caused by sudden thermal pressure drops, ensuring zero internal lens fogging.
2. Metal Fabrication & Heavy Machinery Works
In heavy manufacturing zones across Rakovica and Železnik, airborne oil mist and micro-metallic dust present severe hazards to standard lights. Our sealed ADC12 high bay fixtures feature anti-static powder-coated surfaces that resist airborne residue build-up, preserving high heat dissipation and preventing thermal throttling.
3. Chemical & Hazardous Material Storage
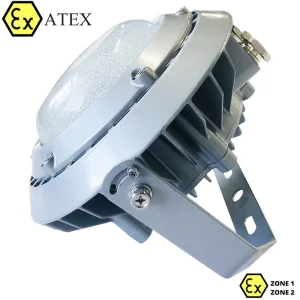
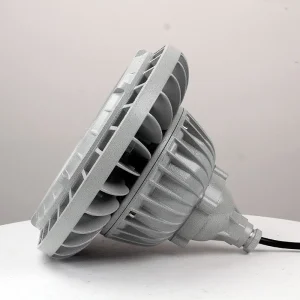
For processing facilities handling volatile organics or chemical raw materials, equipment safety is mandatory. We provide specialized ATEX-certified Zone 1 and Zone 2 explosion-proof high bay luminaires constructed with spark-free cast enclosures and explosion-resistant glass optics to eliminate ignition risks.
Explore our full line of IP65/IP66 high-bay lamps, tri-proof lights, and explosion-proof solutions certified for export to Serbia and European markets.
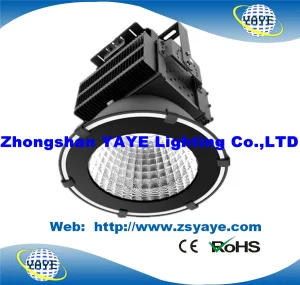
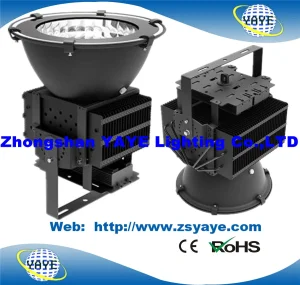
Yaye 18 Waterproof IP65 CE/RoHS 100W LED High Bay Light / 100W LED Industrial Lamp with 5 Years Warranty
Compliance, Regulatory Standards & Local Support for Serbia
Navigating customs, technical documentation, and quality standards for seamless procurement in Belgrade.
AAA EU & Serbian Conformity (AAA / CE Mark)
All industrial lighting systems exported to Belgrade comply fully with European Low Voltage Directives (LVD), Electromagnetic Compatibility (EMC), and RoHS environmental standards. Products carry valid TUV GS, CE, and SAA certifications required for rapid customs clearance through Serbian customs authority endpoints.
Fast Maritime & Overland Supply Routes
Situated merely 38 kilometers from Ningbo Port, our manufacturing plant initiates swift maritime shipping to Southern European hubs (Piraeus, Rijeka, or Bar), supported by direct overland transport corridors into Belgrade. Bulk procurement contracts feature customized packing designed to protect fixtures across multi-modal journeys.
Direct technical and logistical answers for industrial lighting engineers, contractors, and procurement officers.
Q1: Why is IP66 rating critical for industrial high bay lights in Belgrade?
Belgrade experiences extreme seasonal microclimates, ranging from high summer ambient heat to severe winter freezing and damp river valley fog. In industrial warehouses and plants, ambient moisture combined with airborne dust can penetrate standard IP54 lights, causing internal electrical short-circuiting or rapid thermal breakdown. IP66 rating guarantees total dust-tight protection and resistance against powerful water jets, protecting your investment.
Q2: What driver and LED chip configurations are used for thermal endurance?
We integrate premium high-efficiency drivers (MeanWell, Inventronics, or Lifud) paired with high-lumen SMD2835 or SMD3030 LED chips on heavy copper PCB substrates. These components are specified for operation up to +55°C ambient temperatures with 10kV surge protection, protecting the luminaire against power grid fluctuations common in industrial zones.
Q3: Can your factory support custom photometrics (DIALux simulation) for local projects?
Yes. Our engineering R&D center provides complete photometrics and IES file exports for DIALux calculations. We assist Belgrade project contractors in modeling required lux levels, uniformity ratios, and optimal fixture spacing before order placement.
Q4: How does your factory handle custom OEM/ODM packaging and labeling for Serbian importers?
We offer complete OEM customization, including custom inner packaging, laser-engraved branding on aluminum housings, barcoded master cartons, and multilingual instruction manuals compliant with Serbian trade and safety labeling laws.
Q5: What is the typical lead time and shipping process to Belgrade?
Standard production lead times range from 15 to 25 days depending on quantity and custom options. Located 38 km from Ningbo Port, we dispatch containers directly for ocean transport to European entry ports, with total transit time to Belgrade averaging 30-35 days.
Ready to Upgrade Your Industrial Lighting Infrastructure?
Contact our expert engineering team today to receive a comprehensive factory-direct quote, DIALux simulation support, or physical sample evaluation for your Belgrade project.
 Ledlot Lighting